Skip to product information
1 of 5

FYID-Feiyide

FYID FXM-G219 All-Position MIG Pipe Welding System | FXM50 Pro Power Source

FYID FXM-G219 All-Position MIG Pipe Welding System | FXM50 Pro Power Source

Regular price $26,290.00
Regular price Sale price $26,290.00
Sale Sold out
Shipping calculated at checkout.
View full details
Heavy-duty track-type orbital MIG welding · ≥φ219mm

FXM-G219 Heavy-Duty Track-Type Orbital Welding System.

Intelligent automatic MIG orbital welding for large-diameter, heavy-wall pipe. Spring-steel track installs in under 1 minute. 12/24-zone partition control covers all-position 5G girth welds from φ219mm to unlimited diameter, wall thickness 5–100mm.

FCA Luoyang · scoped quote on request
Pipe range ≥ φ219 mm (8.62″) · wall 5–100 mm
Process MIG (GMAW)
Power source FXM50 Pro · confirm by configuration
Control Wireless / WiFi · 5-inch touchscreen · 12/24 zones
Compliance ISO 9001 · No usable CE certificate at present · Alibaba Gold Plus (SGS-verified, valid Dec 2026)
Warranty 12 months whole-machine (excl. consumables)
01 / What it is

A track-type automatic MIG orbital welder for pipes ≥ φ219mm — from oil & gas field joints to power plant steam headers.

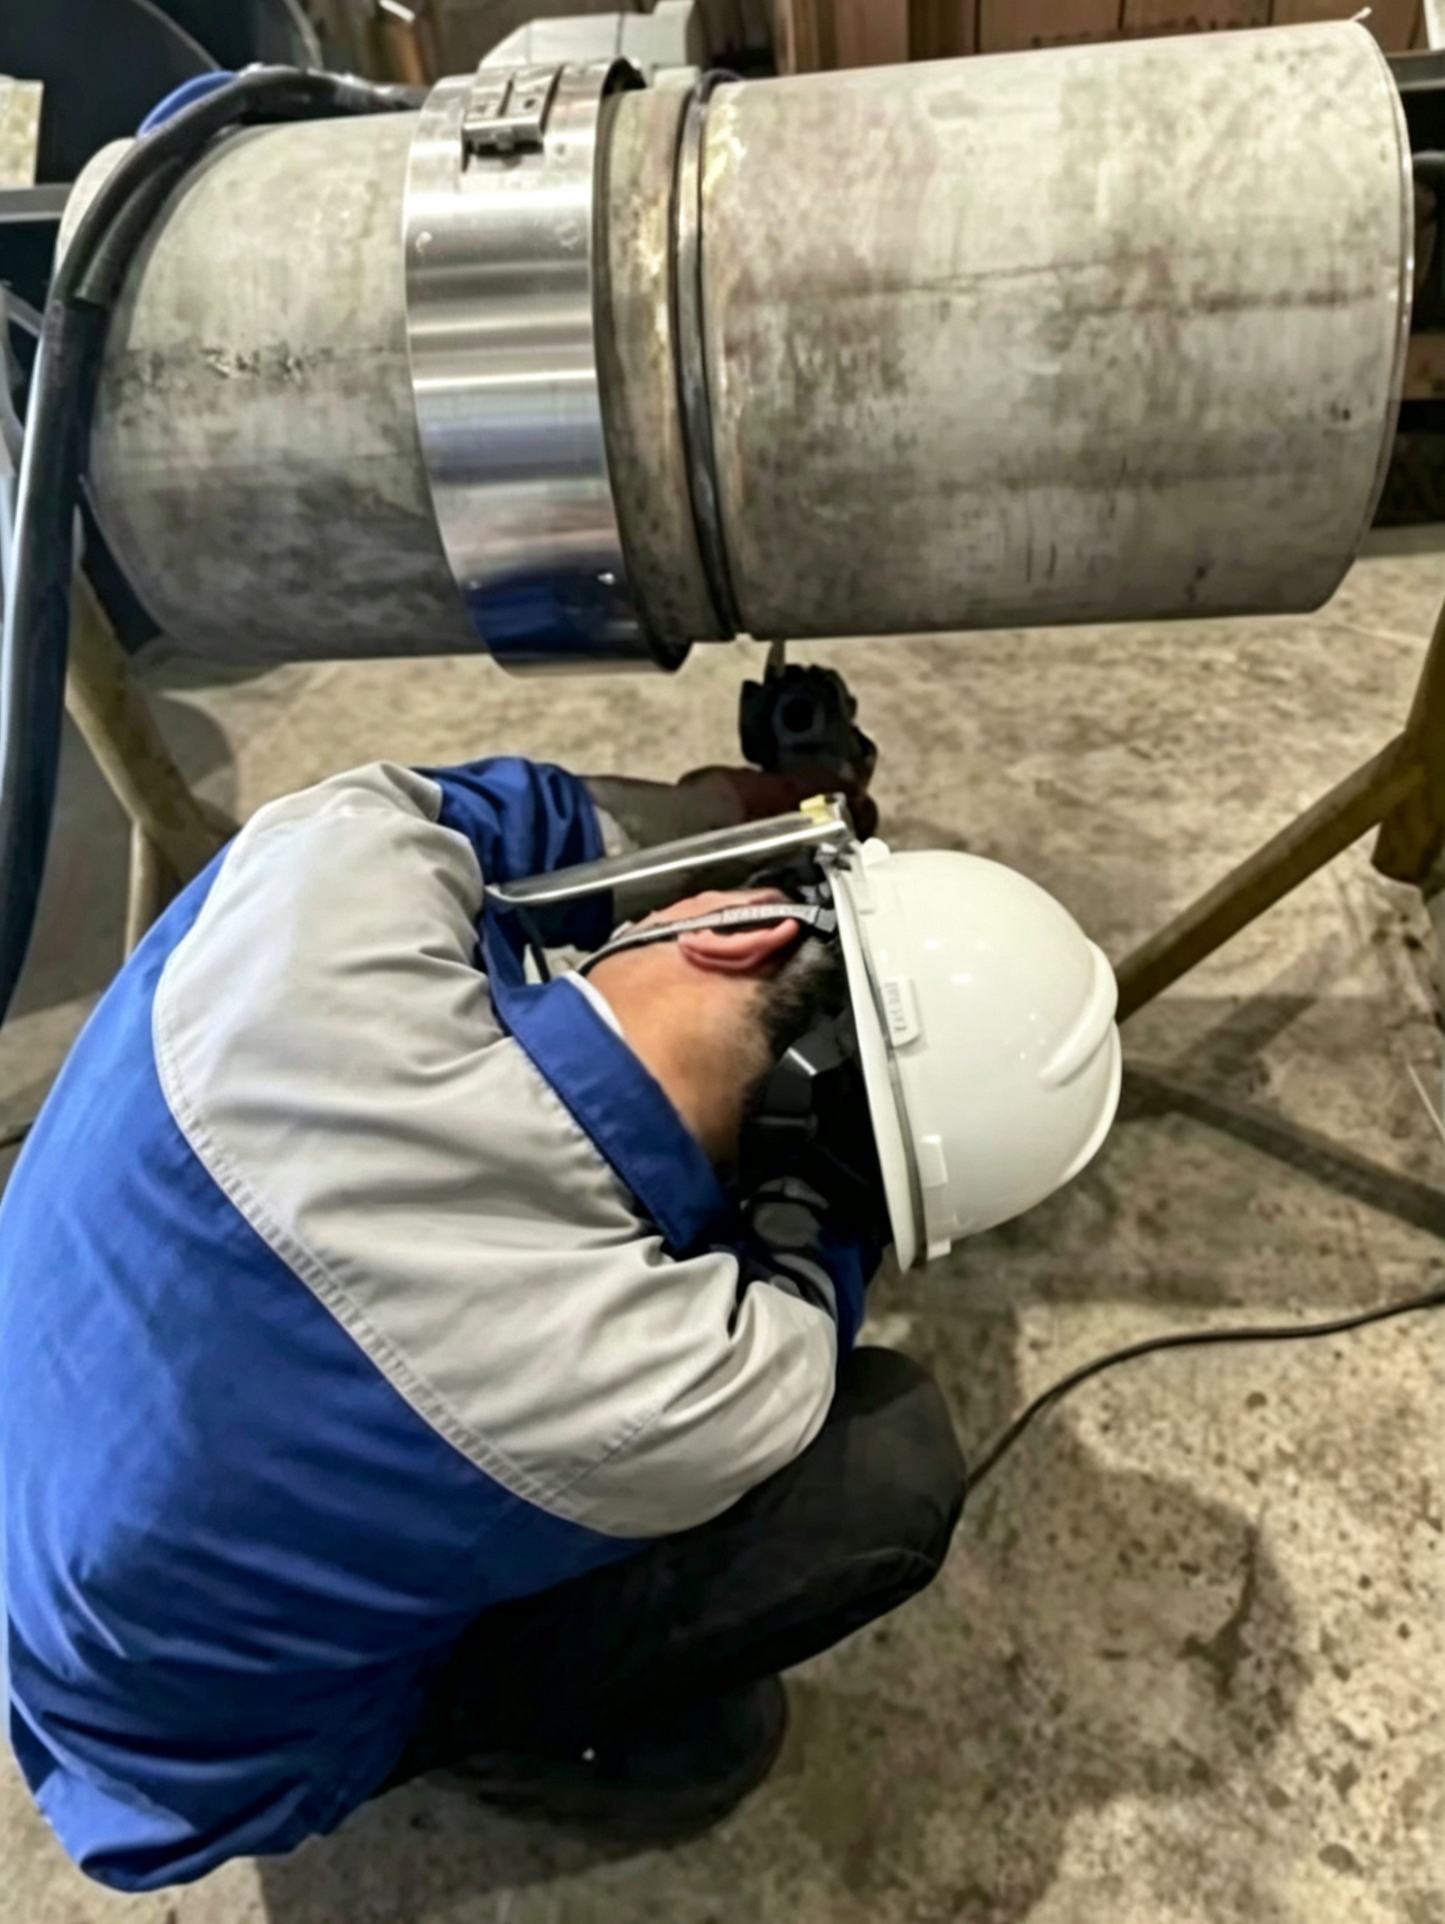
The FXM-G219 is a track-type intelligent automatic MIG orbital welding system designed for large-diameter, heavy-wall pipe girth welding. The FXM-G219 welding head rides a customized spring-steel track that clips around the pipe OD in under 1 minute and is removed without damaging the pipe surface or insulation layer. The head travels the full 360° circumference while the pipe remains stationary — covering flat, horizontal, vertical, and overhead positions in a single uninterrupted pass.

Unlike K-series clamp heads (φ20–325mm) that grip as a rigid chuck assembly, the FXM-G219 track system is built for pipes where a clamp cannot physically close or grip — starting at φ219mm and scaling to any diameter the project requires. Track geometry is customized per pipe OD; standard track lead time is 10–20 working days.

The system pairs with the FXM50 Pro power source: an industrial MIG power supply with electrical ratings to confirm with wireless 5-inch control, integrated wire feeder, and an air-cooled host. The separate FXT40 Pro and FXM50 Pro power sources drive the K-series modular clamp heads (φ20–325mm) and the FXM-G219 track-type head — a pipeline contractor’s fleet covers the full pipe size range from separate power sources and model-specific program libraries.

12/24-zone intelligent partition control

A built-in angle sensor divides the 360° weld into 12 or 24 independent zones. As the head travels around the pipe, the system automatically adjusts current, travel speed, oscillation width, oscillation speed, and left/right dwell time at each zone boundary — compensating for the thermal and gravitational asymmetry between the flat position (6 o’clock) and the overhead position (12 o’clock). Operators configure zone parameters via wireless remote control before welding starts and fine-tune in real time without stopping the weld.

AVC arc length tracking

Integrated AVC (Automatic Voltage Control) maintains constant arc length in real time, compensating for pipe out-of-roundness, thermal expansion between passes, and track deviation. Control precision: arc length variation < ±0.1 mm (confirm by configuration) at < 10 ms (confirm by configuration) response time. On heavy-wall pipe where root-pass penetration is the most sensitive quality variable, AVC is the system’s primary quality assurance mechanism.

02 / Key capabilities

What the FXM-G219 system does that manual welding cannot.

3–4× faster

Faster than manual SMAW; approximately 2× faster than manual TIG. Travel speed continuously adjustable from 50 to 900 mm/min. On large-bore pipeline construction, this shortens project schedules directly.

12/24-zone control

Automatic per-zone parameter adjustment for flat, horizontal, vertical, and overhead positions in one rotation. Handles 5G all-position fixed-pipe welding without operator intervention at each position change.

AVC arc tracking

Compensates for pipe out-of-roundness, thermal growth between passes, and track deviation in real time. Arc length variation < ±0.1 mm (confirm by configuration) at < 10 ms (confirm by configuration) response — the root pass achieves consistent penetration regardless of pipe geometry.

110mm (confirm by configuration) narrow track

Track width is only 110mm (confirm by configuration). Installs on thermally insulated pipe without removing the insulation layer — saving stripping, reinstallation, and insulation replacement costs on maintenance and turnaround projects.

Wireless remote

All parameters (current, speed, oscillation, AVC voltage) adjustable via wireless remote during welding without interruption. One-hand ergonomic operation; the operator stays clear of the arc and spatter zone.

Extreme duty range

Operating temperature −20°C to +60°C (head) / −20°C to +60°C (system). Anti-interference communication. Designed for long-distance pipeline construction, buried field joints, and offshore platform work beyond the range of shop-based equipment.

Cold wire option

Integrated wire feeder for heavy-wall pipe (≥ 5mm) fill and cap passes. Wire feeding speed 0–2500 mm/min; accepts 1.0 / 1.2 mm wire. Increases deposition rate without proportionally increasing heat input.

Digital traceability

model-specific recipe storage. Per-weld data log: current, voltage, travel speed, oscillation parameters, timestamp. Supports ISO audit and pipeline code compliance documentation on ASME / API 1104 projects.

03 / Engineering specifications

Spec sheet for procurement.

Welding process
MIG / GMAW
Pipe OD range
≥ φ219 mm (8.62″) · no upper limit (track customized per project)
Wall thickness
5–100 mm
Materials
Carbon steel · stainless 304 / 316 / 316L · alloy steel · low-temperature steel · titanium alloy · duplex stainless
Welding head (FXM-G219)
Weight 11 kg · DC 12–35 V operating voltage (typical 24 V) · rated power < 100 W
Travel speed
50–900 mm/min (continuous)
Current range
FXM-G219: 80–500 A · FXM50 Pro: confirm by configuration
AVC voltage range
16–35 V (FXM-G219)
Oscillation speed
0–50 mm/s
Oscillation width
2–30 mm
Head angle adjustment
±15°
Dwell time (each side)
0–2 s
Wire feeding speed
0–2500 mm/min
Filler wire diameter
1.0 / 1.2 mm
Tungsten electrode
N/A (MIG)
Zone partition control
12 zones or 24 zones (360° partition, angle sensor-based)
Stored programs
confirm by configuration
Track width
confirm by configuration
Track installation time
confirm by configuration
Head dimensions (without wire feeder)
24×31×23 cm
Head dimensions (with wire feeder)
44×31×24 cm
Power source (FXM50 Pro)
FXM50 Pro · confirm by configuration
Power source weight
confirm by configuration
Power source dimensions
confirm by configuration
Control system
Wireless / WiFi · 5-inch touchscreen
Cooling
Air-cooled (FXM50 Pro) · confirm by configuration
Operating temperature
−20°C to +60°C (FXM-G219) · FXM50 Pro: confirm by configuration
Certifications
ISO 9001 · No usable CE certificate at present · Alibaba Gold Plus (SGS, valid Dec 2026)
Standards fit
ASME Section IX · API 1104 · ISO 13847 · EN ISO 15614 · GB/T 985
Warranty
12 months whole-machine · consumables excluded · lifetime technical support after warranty
04 / Industry use cases

Where the FXM-G219 fits.

→ Oil & Gas Pipeline

Long-distance pipeline field joints and buried tie-ins.

Long-distance liquid and gas transmission pipelines require thousands of field girth welds on fixed horizontal pipe at temperatures ranging from arctic permafrost to desert summer. Manual SMAW is the historical norm; the FXM-G219 replaces it with automatic MIG orbital welding at 3–4× the speed, with consistent root penetration confirmed by AVC that compensates for pipe ovality and field-induced track deviation.

The 110mm (confirm by configuration) narrow track installs on pipe in the field in under 1 minute without scaffolding adjustment or insulation removal. The wireless remote lets the operator monitor the weld from a safe distance, adjusting parameters per zone as thermal buildup on multi-pass thick-wall sections requires current reduction.

Materials: API 5L X42 / X52 / X65 / X70 carbon steel line pipe. Wall range: 5–100mm. Codes: API 1104, ASME B31.4 (liquid pipeline), ASME B31.8 (gas pipeline), ISO 13847.

→ Power Generation

Nuclear and thermal power plant main steam and feedwater piping.

Nuclear power plants and thermal power stations use large-bore, thick-wall alloy steel pipe (SA-335 P91, P22, P11) for main steam and feedwater headers. These joints operate at 5–25 MPa and 350–600°C — service conditions where weld quality is a safety-critical requirement. The FXM-G219’s AVC + 12/24-zone control delivers the per-joint consistency that manual welding cannot match across hundreds of joints. Per-weld data logging supports 10 CFR 50 Appendix B and NQA-1 traceability requirements for nuclear auxiliary piping.

Materials: SA-335 P11 / P22 / P91 chrome-moly alloy steel, SA-106 carbon steel, 316L for auxiliary lines. Codes: ASME Section I (Power Boilers), ASME B31.1 (Power Piping), ASME Section IX, NQA-1.

→ Petrochemical & Refinery

Refinery main process headers and transmission piping.

Large-bore process pipe in refineries — main headers, transfer lines, and reactor inlet/outlet piping — presents thick walls requiring multi-pass fill, alloy grades requiring preheating, and turnaround windows of 4–6 weeks that compress hundreds of joints into a fixed schedule. The FXM-G219 delivers consistent root pass quality via AVC, with multi-pass fill and cap parameters per zone stored in the model-specific recipe library for instant operator recall.

Materials: Carbon steel (SA-106 B/C), chrome-moly (P11/P22), stainless 304/316L, duplex 2205. Codes: ASME B31.3, API 570, API 510.

→ Shipbuilding & Offshore

Offshore platform piping and large-bore marine pipe systems.

Offshore platform construction involves large-bore carbon steel and 316L stainless pipe installed in confined spaces at elevation, often in variable weather. The FXM-G219 system operates across −20°C to +60°C ambient with anti-interference wireless communication that maintains stability in the RF-dense environment of an active fabrication yard. Per-weld parameter logs satisfy classification society (DNV-GL, ABS, Lloyd’s Register) joint traceability requirements.

Materials: Carbon steel marine grade, stainless 316L, duplex 2205 for sour service. Codes: DNV-GL, ABS, Lloyd’s Register, CCS, ASME Section IX, ISO 15614.

05 / Procurement questions

What buyers ask before the PO.

What pipe diameters can the FXM-G219 handle?

The FXM-G219 track-type system is designed for pipes ≥ φ219mm (≥ 8.62 inches). There is no upper diameter limit — the spring-steel track is customized per project OD. Standard track lead time is 10–20 working days. For pipes up to φ325mm where a clamp-head assembly is practical, the FXT40 Pro + K-series (K219 / K325) provides shorter lead time without custom track fabrication.

Can it weld stainless steel and alloy steel pipe?

Yes. The system supports carbon steel, stainless steel (304, 316, 316L, duplex 2205), alloy steel, low-temperature steel, and titanium alloy. Configured MIG/GMAW modes are available. For stainless steel and high-purity process piping, the procedure-qualified MIG process delivers a clean bead surface with post-weld finishing confirmed by the procedure.

How does the track install? Does it require removing pipe insulation?

The spring-steel track snaps around the pipe OD in under 1 minute and locks in place without surface damage. Track width is only 110mm (confirm by configuration) — narrow enough to install on thermally insulated pipes without removing the insulation layer. This saves stripping, reinstallation, and replacement costs on maintenance and turnaround projects where insulation removal is a significant additional cost.

How fast is it compared to manual welding?

The FXM-G219 system is 3–4× faster than manual SMAW (stick welding) and approximately 2× faster than manual TIG. Travel speeds range continuously from 50 to 900 mm/min. The intelligent 12/24-zone partition control maintains weld quality at these speeds without the fatigue-related inconsistency that limits manual orbital welders on heavy-wall pipe.

Can it operate in field conditions — cold weather, outdoor environments?

Yes. System operating range is −20°C to +60°C for the welding head and −20°C to +60°C for the overall system. Anti-interference wireless communication maintains reliable performance in outdoor and industrial environments. The system is routinely used for long-distance pipeline construction, buried pipeline field joints, and offshore platform piping.

Does it share the same FXT40 Pro power source as the K-series heads?

No. The FXM-G219 welding head uses the separate FXM50 Pro power source from the K-series modular clamp heads. A pipeline contractor operating both diameter ranges — K-series (φ20–325mm) for instrumentation and process lines, FXM-G219 track-type for main transmission pipe — uses separate power source platforms and model-specific recipe libraries across the full project scope.

What does the 12/24-zone partition control actually do?

A built-in angle sensor divides the 360° weld circumference into 12 or 24 independent zones. At each zone boundary, the system automatically adjusts welding current, travel speed, oscillation width, oscillation speed, and left/right dwell time — compensating for how gravity affects the molten weld pool differently at flat (6 o’clock), vertical (3 and 9 o’clock), and overhead (12 o’clock) positions. The operator configures parameters for each zone and each layer via wireless remote control before welding starts, and can fine-tune in real time during the pass.

→ Related

Other systems in the FYID-Feiyide range.

重型履带式轨道MIG焊接 · ≥φ219mm

FXM-G219重型履带式轨道焊接系统。

用于大口径、厚壁管道的智能自动MIG轨道焊接。弹簧钢履带不足1分钟即可安装。12/24分区控制覆盖从φ219mm到任意直径、壁厚5–100mm的全位置5G环形焊缝。

FCA洛阳 · 按需报价
管道范围 ≥φ219 mm(8.62")· 壁厚5–100 mm
焊接工艺 MIG (GMAW)
电源 FXM50 Pro · 按配置确认
控制 Wireless / WiFi · 5-inch touchscreen · 12/24 zones
认证 ISO 9001 · 目前无可用CE证书 · 阿里巴巴金牌(SGS核验,有效期至2026年12月)
质保 整机12个月(耗材除外)
01 / 产品介绍

适用于≥φ219mm管道的履带式自动MIG轨道焊机——从油气现场接头到电厂蒸汽集管。

FXM-G219是专为大口径厚壁管道环形焊接设计的履带式智能自动MIG轨道焊接系统。FXM-G219焊头安装在定制弹簧钢履带上,履带可在1分钟内卡扣固定于管道外径,拆除时不损伤管道表面或保温层。焊头沿360°管道圆周运行,管道保持固定——在一次连续焊接中覆盖平焊、横焊、立焊和仰焊位置。

与K系列夹具焊头(φ20–325mm)不同,FXM-G219履带系统专为夹具无法物理夹紧或锁定的管道而设计——从φ219mm起,可扩展至项目所需的任意直径。履带几何形状按管道外径定制,标准履带交货期10–20个工作日。

该系统与FXM50 Pro电源配套使用:电气额定值待确认的MIG/GMAW电源,配备无线WiFi五英寸触摸屏控制、集成数字送丝机以及风冷主机及冷却配置待确认的焊头。FXT40 Pro电源驱动K系列模块化夹具焊头(φ20–325mm),FXM50 Pro电源驱动FXM-G219履带式焊头——管道承包商的设备可通过两款电源平台和分型号配方库覆盖全管径范围。

12/24区段智能分区控制

内置角度传感器将360°焊缝分为12或24个独立区段。焊头绕管道运行时,系统在每个区段边界自动调整电流、行走速度、摆动幅度、摆动速度和左右停留时间——补偿平焊位置(6点钟)和仰焊位置(12点钟)之间的热量和重力不对称。操作者在焊接开始前通过无线遥控器配置各区段参数,并可在焊接过程中实时微调,无需停机。

AVC弧长跟踪

集成AVC(自动电压控制)实时维持恒定弧长,补偿管道椭圆度、多层焊道间热膨胀和履带偏差。控制精度:弧长变化量<±0.1 mm (按配置确认),响应时间<10 ms (按配置确认)。对于厚壁管道——根部熔透是最敏感的质量变量——AVC是系统的主要质量保障机制。

02 / 核心能力

FXM-G219系统能做到而手工焊接做不到的事。

速度提升3–4倍

比手工焊条电弧焊(SMAW)快3–4倍,比手工TIG约快2倍。行走速度50–900 mm/min连续可调。在大口径管道施工中,直接缩短项目工期。

12/24分区控制

单次旋转中自动按区段调整平焊、横焊、立焊和仰焊位置参数。固定管道5G全位置焊接无需操作者在每个位置变化时干预。

AVC弧长跟踪

实时补偿管道椭圆度、多层焊道间热膨胀和履带偏差。弧长变化量<±0.1 mm (按配置确认),响应时间<10 ms (按配置确认)——无论管道几何形状如何,根部焊道均实现一致熔透。

110mm (按配置确认)窄型履带

履带宽度仅110mm (按配置确认)。可安装在有保温层的管道上,无需拆除保温——节省维修和大修项目中的剥除、重装和更换保温的费用。

无线遥控

焊接过程中所有参数(电流、速度、摆动、AVC电压)均可通过无线遥控器调整,无需中断。单手人体工学操作,操作者可远离弧光和飞溅区。

极端工况适应性

工作温度-20°C至+60°C(焊头)/−20°C to +60°C(系统)。抗干扰通信。专为长距离管道施工、埋地现场接头和超出车间设备作业范围的海上平台作业设计。

冷丝送丝选项

集成送丝机,用于厚壁管道(≥5mm)的填充和盖面焊道。送丝速度0–2500 mm/min,接受1.0 / 1.2 mm焊丝。在不成比例增加热输入的情况下提高熔敷效率。

数字化溯源

按配置确认的配方存储。每焊口数据记录:电流、电压、行走速度、摆动参数、时间戳。支持ASME/API 1104项目的ISO审计和管道规范合规文件。

03 / 工程规格

采购规格表。

焊接工艺
MIG / GMAW
管道外径范围
≥φ219 mm(8.62")· 无上限(履带按项目定制)
壁厚
5–100 mm
材质
碳钢 · 不锈钢304/316/316L · 合金钢 · 低温钢 · 钛合金 · 双相不锈钢
焊头(FXM-G219)
重量11 kg · DC 12–35 V工作电压(典型24 V)· 额定功率<100 W
行走速度
50–900 mm/min(连续可调)
电流范围
FXM-G219: 80–500 A · FXM50 Pro: 按配置确认
AVC电压范围
16–35 V (FXM-G219)
摆动速度
0–50 mm/s
摆动幅度
2–30 mm
焊头角度调节
±15°
两侧停留时间
0–2 s
送丝速度
0–2500 mm/min
填充焊丝直径
1.0 / 1.2 mm
钨极
N/A (MIG)
分区控制
12区或24区(360°分区,角度传感器控制)
存储程序
按配置确认
履带宽度
按配置确认
履带安装时间
按配置确认
焊头尺寸(不含送丝机)
24×31×23 cm
焊头尺寸(含送丝机)
44×31×24 cm
电源(FXM50 Pro)
FXM50 Pro · 按配置确认
电源重量
按配置确认
电源尺寸
按配置确认
控制系统
Wireless / WiFi · 5-inch touchscreen
冷却方式
风冷 (FXM50 Pro) · 按配置确认
工作温度
−20°C to +60°C (FXM-G219) · FXM50 Pro: 按配置确认
认证
ISO 9001 · 目前无可用CE证书 · 阿里巴巴金牌(SGS,有效期至2026年12月)
标准符合性
ASME Section IX · API 1104 · ISO 13847 · EN ISO 15614 · GB/T 985
质保
整机12个月 · 耗材除外 · 质保期后终身技术支持
04 / 行业应用场景

FXM-G219的适用领域。

→ 油气管道

长距离管道现场接头与埋地连接焊缝。

长距离液体和气体输送管道需要在固定水平管道上完成数千道现场环焊缝,作业温度从北极冻土到沙漠夏季不等。手工焊条电弧焊是传统做法;FXM-G219以3–4倍的速度取而代之,通过AVC补偿管道椭圆度和现场导轨偏差,确保根部焊道熔透质量。

110mm (按配置确认)窄型履带可在现场1分钟内安装于管道上,无需调整脚手架或拆除保温层。无线遥控器让操作者可在安全距离外监测焊接,在多层厚壁焊接热量积累需要降低电流时按区段调整参数。

材质:API 5L X42/X52/X65/X70碳钢线管。壁厚范围:5–100mm。标准:API 1104、ASME B31.4(液体管道)、ASME B31.8(气体管道)、ISO 13847。

→ 电力行业

核电和火电厂主蒸汽及给水管道。

核电站和火力发电站使用大口径厚壁合金钢管(SA-335 P91、P22、P11)作为主蒸汽和给水集管。这些接头在5–25 MPa、350–600°C的工况下运行——焊缝质量是安全关键要求。FXM-G219的AVC+12/24分区控制提供手工焊接无法在数百道接头上实现的一致性。每焊口数据记录支持核辅助管道10 CFR 50附录B和NQA-1溯源要求。

材质:SA-335 P11/P22/P91铬钼合金钢、SA-106碳钢、辅助管道用316L。标准:ASME Section I(动力锅炉)、ASME B31.1(动力管道)、ASME Section IX、NQA-1。

→ 石化与炼油

炼油厂主工艺集管和输送管道。

炼油厂大口径工艺管道——主集管、转输管线和反应器进出口管道——具有需要多层填充的厚壁、需要预热的合金钢牌号,以及将数百道接头压缩进固定时间的4–6周大修窗口期。FXM-G219通过AVC保证一致的根部焊道质量,多层填充和盖面焊道的按区段参数存储在按配置确认的配方库中供操作者即时调用。

材质:碳钢(SA-106 B/C)、铬钼钢(P11/P22)、不锈钢304/316L、双相钢2205。标准:ASME B31.3、API 570、API 510。

→ 船舶与海洋工程

海上平台管道和大口径船用管道系统。

海上平台建造涉及在高空受限空间安装大口径碳钢和316L不锈钢管道,通常在多变天气条件下作业。FXM-G219系统在−20°C to +60°C环境温度下运行,抗干扰无线通信在活跃建造场地的高射频密度环境中保持稳定。每焊口参数记录满足船级社(DNV-GL、ABS、劳氏船级社)接头溯源要求。

材质:船用级碳钢、316L不锈钢、酸性服役用双相钢2205。标准:DNV-GL、ABS、劳氏船级社、CCS、ASME Section IX、ISO 15614。

05 / 采购常见问题

采购商下单前的常见问题。

FXM-G219能处理多大管径?

FXM-G219履带式系统专为≥φ219mm(≥8.62英寸)管道设计。无外径上限——弹簧钢履带按项目外径定制。标准履带交货期10–20个工作日。对于φ325mm以内、夹具组件可实际夹紧的管道,FXT40 Pro+K系列(K219/K325)交货期更短,无需定制履带。

能焊接不锈钢和合金钢管道吗?

可以。系统支持碳钢、不锈钢(304、316、316L、双相钢2205)、合金钢、低温钢和钛合金。MIG/GMAW模式均可用。对于不锈钢和高纯度工艺管道,按规程确认的MIG工艺产生洁净的焊道表面,焊后处理按规程确认。

履带如何安装?是否需要拆除管道保温?

弹簧钢履带1分钟内卡扣固定于管道外径,锁定时不损伤表面。履带宽度仅110mm (按配置确认)——窄到可在有保温层的管道上安装而无需拆除保温。这为维修和大修项目节省了剥除、重装和更换保温的费用——这些费用通常相当可观。

与手工焊接相比速度如何?

FXM-G219系统比手工焊条电弧焊快3–4倍,比手工TIG约快2倍。行走速度50–900 mm/min连续可调。智能12/24分区控制在保持高速的同时维持焊缝质量,避免厚壁管手工轨道焊接中因疲劳导致的不一致性。

能在现场条件下作业——寒冷天气、户外环境?

可以。系统工作范围:焊头-20°C至+60°C,整体系统−20°C to +60°C。抗干扰无线通信在户外和工业环境中保持可靠性能。该系统常规用于长距离管道施工、埋地管道现场接头和海上平台管道作业。

与K系列焊头共用同一台FXT40 Pro电源吗?

不是。FXM-G219焊头使用与K系列模块化夹具焊头不同的FXM50 Pro电源。同时运营两种管径范围的管道承包商——K系列(φ20–325mm)用于仪表和工艺管线,FXM-G219履带式用于主输送管道——使用两款电源平台和分型号确认的配方库覆盖全项目范围。

12/24分区控制实际做什么?

内置角度传感器将360°焊缝圆周分为12或24个独立区段。在每个区段边界,系统自动调整焊接电流、行走速度、摆动幅度、摆动速度和左右停留时间——补偿重力对平焊(6点钟)、立焊(3和9点钟)和仰焊(12点钟)位置熔池的不同影响。操作者在焊接开始前通过无线遥控器配置每个区段和每个焊道的参数,并可在焊接过程中实时微调。

→ 相关产品

FYID-Feiyide产品系列中的其他系统。

Contact us for a quote