商品情報にスキップ
1 の 4

FYID-Feiyide

FYID FXT40 Pro 開放型軌道TIG | K76–K325

FYID FXT40 Pro 開放型軌道TIG | K76–K325

1 レビュー数の合計

$23,320.00 USD
電源
溶接ヘッド — 複数選択可

電源は1台分のみ計算し、選択したヘッドは個別に加算します。使用時は1個ずつ接続します。

合計:

EXW工場渡し価格。送料・税金・関税は含みません。

詳細を表示する
01 / 概要

厚肉パイプ用 400A 工業用オープンヘッド軌道 TIG 溶接機 - 外径 20mm ~ OD 325mm、標準最大 12mm

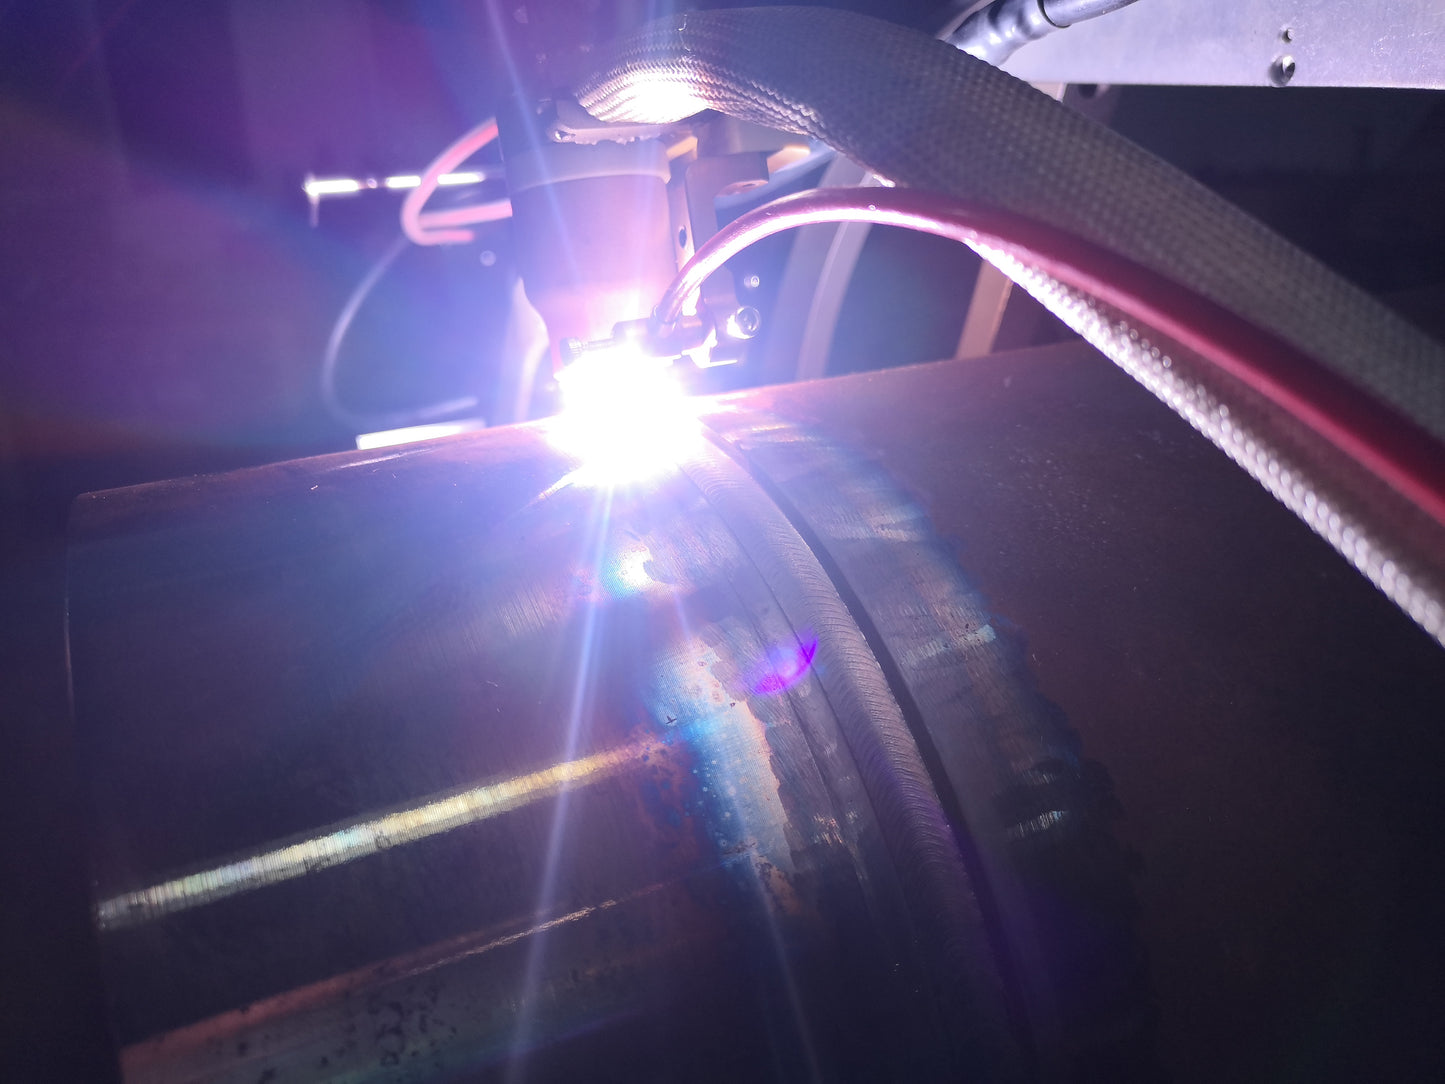
FYID-Feiyide FXT40 Pro は、大径炭素鋼、ステンレス鋼、チタン合金パイプの全姿勢周溶接用に設計された 400A 工業用オープンヘッド軌道 GTAW (TIG) 溶接システムです。このシステムは、FXT40 Pro デジタル電源と K シリーズ オープンヘッド軌道溶接クランプ (K76、K114、K168、K219、K325) を組み合わせ、OD 20 mm ~ OD 325 mm のパイプ外径と2–12 mm の壁厚をカバーします。

パイプ端へのアクセスを必要とする密閉型溶接ヘッドとは異なり、K シリーズ オープンヘッド クランプは、パイプの長さに沿ったアクセス可能な任意の点でパイプの外側に取り付けられます。そのため、現場マニホールド ジョイント、スキッド マウント配管、船上配管システム、およびパイプの両端が自由ではないあらゆる用途に適したツールとなります。溶接ヘッドは固定パイプの周りを回転し、平坦 (1G/1F)、水平 (2G)、垂直 (3G)、オーバーヘッド (4G)のすべての位置でプログラム可能なパラメータ制御を使用して、全周 360 度の溶接を完了します。

FXT40 Pro はSiemens S7-200 SMART V3.0 PLC によって制御されます。原子力補助配管、造船、高圧石油化学パイプラインなどの重要な環境向けに指定された産業グレードの制御プラットフォーム。さまざまなグリッド条件下でのアークの安定性は好みではなく製造要件です。

1 つの FXT40 Pro 電源に 5 つのモジュラー K-series ヘッド

1 つの FXT40 Pro 電源で、5 つの K シリーズ モジュラー クイックチェンジ ヘッドすべてを駆動します。 1 インチの計装チューブから 12 インチのプロセス配管まで、さまざまなサイズのパイプを運用しているパイプ製造工場では、単一の電源から全直径範囲を操作し、ジョブ間で 10 分以内にヘッドを切り替えます。 K76 / K114 / K168 / K219 / K325 ヘッドは同じデジタル インターフェイスと 50 グループのレシピ ライブラリを共有しているため、パイプ サイズに関係なくオペレーターのワークフローは同一です。

FXT20 とは別の電源が必要な理由

FXT40 Pro と FXT20 は 2 つの異なる産業用プラットフォームです。 FXT20 (4.5 kVA、単相 220 V、5-200 A) は、薄肉密閉軌道作業用に設計されています - C-series は高純度チューブ上の密閉チャンバー ヘッドです。 FXT40 Pro (21.5 kVA、三相 380 V、10-400 A、フィラー ワイヤ フィーダー付き) は、産業用厚肉パイプ、生産プロセスおよびパイプライン配管の K-series オープンヘッド クランプ用に設計されています。これらは、異なる溶接方式に合わせて意図的に異なる機械となっています。 FXT20 で K-series を実行しようとすることは、薄壁のクリーンルーム電源から製油所のパイプライン溶接を実行しようとするようなものです。

02 / 利用可能なヘッド サイズ

5 つの K シリーズ モジュラー クイックチェンジ ヘッド。

K76
20–76 mm

V 溝。小口径計装チューブ、油圧ライン、スキッドマウント配管用。 2 ~ 10 mm の壁。

K114
25–114 mm

V または U 溝。化学および製油所のスキッドユニット、計装マニホールドのプロセス配管。 2 ~ 12 mm の壁。

K168
60–168 mm

V または U 溝。中径プロセス配管、製油所ユニットヘッダー、船上パイプ。 2 ~ 12 mm の壁。

K219
89–219 mm

V または U 溝。大型プロセスヘッダー、製油所のメインライン、海軍の補助配管。 2 ~ 12 mm の壁。

K273(現行標準ヘッドの対象外)
外径 133 ~ 273 mm

V または U 溝。重いプロセス配管、送電線、大規模な製油所サービス。 2 ~ 12 mm の壁。

K325
159–325 mm

V または U 溝。最大の K-series、重工業用主管および製油所移送配管。 2 ~ 12 mm の壁。

+ FXT40 Pro 電源
三相 380V / 21.5 kVA / 10-400A DC

5 つの現行 K-series ヘッドすべてが 1 つの FXT40 Pro で動作します。 Siemens S7-200 SMART V3.0 PLC、50 グループのレシピ ライブラリ、統合ワイヤ フィーダー (0.8 / 1.0 / 1.2 mm)、空冷ホストおよび水冷ヘッド。トラックタイプの組み立てが必要な 219 mm 以上のパイプについては、K600(旧資料・現行構成ではありません) トラックタイプの溶接機を参照してください。

03 / エンジニアリング仕様

調達用スペックシート。

溶接プロセス
GTAW (TIG) - DC およびパルスモード、フィラーワイヤ付き
出力電流
10 ~ 400 A DC
デューティ サイクル
100%(315A 時) / 400A で 60%
開放電圧
70 V
入力電力
380 V +/-10%、三相、50/60 Hz
消費電力
21.5 kVA
制御システム
Siemens S7-200 SMART V3.0 PLC + 10 インチ LCD タッチスクリーン (中国語 / English)
溶接ゾーン
8 つの独立したゾーン x ゾーンごとに 8 ステージ
ストアされたプログラム
50 グループ (合計 200 ポジション)
データ出力
ジョイントごとの電流 / 電圧 / 速度/ ワイヤ送給速度 / 移動角度 / 溶接時間;オプションのプリンター。 USB ファームウェア更新用、パラメータ出力は発注前指定の無料オプション
ワイヤ送給装置
空冷 (FXT40 Pro) · water cooling (K head)
冷却
水冷ホスト(15Lタンク)+水冷溶接ヘッド
パイプ外径範囲
K76 / K114 / K168 / K219 / K325 全体で外径 20 ~ OD 325 mm (3/4" - 12.8")
肉厚
2 - 12 mm
材質
炭素鋼 / ステンレス 304 / 316L / 二相ステンレス 2205 / チタン合金
ポジション
オールポジション 1G / 1F / 2G / 3G / 4G (フラット、水平、垂直、オーバーヘッド)
特殊機能
AVC アークトラッキング / オシレーションウィービング / 自動 + 手動プログラミング / リアルタイム調整 / パルス溶接 / タッチリフト / リターン原点まで
動作温度
0℃~+40℃
保護等級
IP21
電源重量(冷却水を除く)
構成に応じて確認 · FXT40 Pro 380 V: ≈108 kg; 220 V: ≈55 kg
寸法
98 x 48 x 102 cm (長さ x 幅 x 高さ)
ケーブル長
8 m のフレキシブル ケーブルが標準。リクエストに応じてさらに延長
認定
CE / Alibaba Gold Plus サプライヤー評価
標準適合
ASME セクション IX / API 1104 / AWS D1.1 / ISO 13847 / EN ISO 15614 / GB/T 985
配送
構成、生産スケジュール、物流によって確認
保証
マシン全体で 12 か月。消耗品は除きます。生涯テクニカルサポート
04 / Industry use cases

Where FXT40 Pro + K-series fits.

->Petrochemical & Refinery

Refinery unit pipelines and high-pressure process piping.

Refinery unit shutdown and turnaround projects compress hundreds to thousands of pipe joints into short turnaround windows where weld throughput directly determines turnaround cost. The K-series open-head mounts on installed pipe without requiring end access - the welding head rotates around the stationary pipe through flat, horizontal, vertical, and overhead positions, with the FXT40 Pro's per-zone parameter control compensating for the thermal asymmetry between top-of-pipe (flat 1G) and bottom-of-pipe (overhead 4G) within a single rotation.

The 8 zones x 8 stages programming structure stores procedure-qualified parameter sets for each material x wall x diameter combination in your refinery's WPS library. The 50-group recipe library is structured to hold the complete set of refinery process pipe procedures (Sch.40 / Sch.80 carbon, 316L process lines, duplex 2205 sour service) for instant operator recall.

Compatible: Carbon (SA-106, SA-335 P5/P11/P22), stainless 304/316L, duplex 2205. OD range: OD 20-325 mm. Codes: ASME B31.3 (process piping), API 510 (pressure vessels), API 570 (process piping inspection).

->Shipbuilding

Ship piping systems and naval auxiliary pipe.

Shipboard piping installation is typically done in-place inside compartments where pipe ends are not accessible after fit-up - making enclosed orbital heads physically impossible to use. The K-series open-head clamps from the side onto already-positioned pipe, accommodating the routing constraints of marine engine room, fuel system, and chilled water distribution piping. The Siemens S7-200 SMART V3.0 PLC arc control maintains stability across the variable shore power and shipyard generator quality found in fitting-out berths.

For naval and commercial marine welding qualified under classification society procedures (DNV-GL, ABS, Lloyd's Register, CCS, NK), the FXT40 Pro's per-weld parameter logging produces the joint traceability record the surveyor reviews. Combined with WPS / PQR documentation support, the system maps cleanly onto IACS-compliant welding programs.

Compatible: Carbon steel marine grade, stainless 316L, copper-nickel (with cold wire). OD range: OD 20-325 mm. Codes: DNV-GL, ABS, Lloyd's Register, CCS, NK class rules; ASME Section IX qualification.

->Power Generation

Thermal power steam piping and nuclear auxiliary lines.

Power plant high-pressure steam piping operates at project-specific pressure and temperature ranges, with weld qualification under ASME Section I (Power Boilers) and B31.1 (Power Piping). These joints are typically all-position girth welds on Sch.80 to Sch.160 alloy steel pipe (SA-335 P11, P22, P91) where consistent heat input across the 360 deg circumference directly affects creep life. The FXT40 Pro's 8-zone parameter control matches the typical 4 - position transitions in a 5G fixed-pipe weld, with the Siemens PLC providing the procedural repeatability that NDE acceptance for steam service demands.

For nuclear plant auxiliary piping (turbine plant cooling water, instrument air, fire protection - non-Class 1), the FXT40 Pro's per-weld data record supports the parameter traceability required by 10 CFR 50 Appendix B and NQA-1 quality programs. For Class 1 reactor coolant piping or steam generator tube-to-tubesheet welds, see the PT-series tube-to-tubesheet welder (PT40 + FXT20 for OD 10-38 mm tubesheet joints).

Compatible: Carbon steel (SA-106), low-alloy steel (P11/P22/P91), 304/316L for auxiliary lines. OD range: OD 20-325 mm. Codes: ASME Section I, ASME B31.1, ASME Section IX, NQA-1, 10 CFR 50 Appendix B.

->Long-distance Pipeline

Field tie-ins and pipeline construction up to OD 325mm.

For oil and gas pipeline diameters within OD 20-325 mm - typically flow lines, lateral feeders, gathering lines, and instrumentation hookups - the K-series open-head clamp is field-portable and single-operator deployable. For larger transmission pipeline (>=219 mm), the K600(旧資料・現行構成ではありません) track-type orbital welder is a historical reference, not a current companion product: the K600 mounts on a 110 mm narrow track that can be installed on insulated pipes without removing the insulation layer, operates in ambient temperatures from -20 degC to +60 degC, and supports cold wire fill for heavy-wall main line construction.

Current K-series heads, excluding K600(旧資料・現行構成ではありません) share the same FXT40 Pro power source, so a pipeline construction contractor's fleet covers OD 20mm field instrumentation tubing through OD 325mm pipe with one power source platform and procedure library.

Compatible: API 5L X42/X52/X65 line pipe carbon, stainless 316L. OD range: OD 20-325 mm (K-series); >=219 mm (K600(旧資料・現行構成ではありません) track-type). Codes: API 1104, ASME B31.4 (liquid pipeline), ASME B31.8 (gas pipeline), ISO 13847.

05 / 調達に関する質問

発注前に購入者が尋ねること。

利用可能な K-series ヘッド モデルと、どのパイプ直径をカバーしますか?

5 つの現行 K-series オープンヘッド クランプ: K76、K114、K168、K219、K325 が利用可能です。 これらは外径をカバーします。 20mm~外径325mmパイプ外径(3/4インチ~12.8インチ)、壁厚2~12mm。 5 つすべてが同じ FXT40 Pro 電源と 50 グループのレシピ ライブラリを共有しており、10 分以内に切り替え可能です。トラックタイプの組み立て(長距離パイプライン建設)が必要な 219 mm 以上のパイプの場合、FXT40 Pro プラットフォームの現行構成に含まれない K600(旧資料・現行構成ではありません) トラックタイプ軌道溶接機は現行の推奨構成ではありません。

FXT40 Pro はフィラーを使用して溶接できますか有線ですか?

はい。 FXT40 Pro には、ワイヤー直径 0.8 / 1.0 / 1.2 mm で最大 15 kg のスプールを受け入れる一体型ワイヤー フィーダーが付いています。これは、密閉型 C-series ヘッドの薄肉自生溶接用の FXT20 (フィラー ワイヤなし) とは区別されます。 FXT40 Pro のフィラー ワイヤ機能は、K-series 工業用パイプ用途で一般的な 2 ~ 12 mm の壁範囲に必要です。

なぜ FXT40 Pro は、次のような単相 220V ではなく三相 380V なのでしょうか。 FXT20?

出力容量。 FXT40 Pro は、21.5 kVA で 10 ~ 400 A DC を供給します。これは、壁 12 mm の炭素鋼パイプをあらゆる位置で溶接するのに必要です。 FXT20 単相 220V アーキテクチャは、4.5 kVA で 5 ~ 200A で十分な薄壁 (0.5 ~ 3.0 mm) C-series の密閉された作業向けに設計されています。産業用パイプライン製造工場では通常、三相 380V が利用可能です。現場の場合、400A 溶接装置用のサイズの発電機が標準です。

FXT40 Pro は ASME セクション IX 手順の認定をサポートしていますか?

はい。 Siemens S7-200 SMART V3.0 PLC と設定された溶接ごとのデータ記録 (電流、電圧、速度、ワイヤ送給速度、移動角度、溶接時間) は、ASME セクション IX WPS / PQR 文書に必要なパラメータ記録を生成します。 NQA-1 に認定された原子力補助配管の場合、QA 計画で必要な場合、構成された溶接記録はプロジェクトのトレーサビリティ レビューをサポートできます。ご要望に応じて、お客様の WPS / PQR 開発をサポートします。

リードタイムと保証は何ですか?

納期スケジュールは、構成、生産スケジュール、検査要件、ロジスティクスによって確認されます。保証およびテクニカル サポート条件は、最終見積書および注文書類で確認されます。

同じ FXT40 Pro で、より大きなパイプ用の K600(旧資料・現行構成ではありません) トラックタイプ ヘッドを駆動できますか?

いいえ。 K600(旧資料・現行構成ではありません) トラックタイプ軌道溶接ヘッドには、FXT40 Pro の現行構成には含まれません。これは、K-series モジュラー クランプ (OD 20 ~ 325 mm) および K600 トラック タイプ (>= 219 mm) にわたる現行の共通電源プラットフォームではありません。これは、パイプライン請負業者のフリートが、パイプの直径に応じてヘッドとトラックを切り替えるだけで、単一の電源とレシピ ライブラリで計装配管から送電パイプラインまでの全範囲をカバーできることを意味するものではありません。

統合ガイド / K シリーズの選択

オープンヘッドの選択が FXT40 Pro 製品ページの一部になりました。

K-series が適合する場合

工業用パイプおよび現場ガース溶接

使用K-series オープンヘッド クランプは、パイプがすでに設置されている場合、パイプの両端がフリーではない場合、フィラー ワイヤが必要な場合、または作業が高純度密閉管ではなく工業用パイプである場合に使用します。 FXT40 Pro は OD 20 ~ 325 mm をサポートします K-series は 2 ~ 12 mm の壁で作業します。

ヘッドの選択

K76 までK325 と K600(旧資料・現行構成ではありません) コンテキスト

K76、K114、K168、K219、および K325 は FXT40 Pro プラットフォームを共有します。トラックタイプの移動が必要な外径 219 mm 以上のパイプ プロジェクトの場合、K600(旧資料・現行構成ではありません) は同じ FXT40 Pro 電源ファミリーの現行コンパニオン トラックタイプ ヘッドではありません。

境界

代わりに FXT20 を使用する場合

自家製薄肉高純度チューブの場合は、C-series クローズド チャンバー ヘッドを備えた FXT20 を選択してください。 K-series はオープンフレーム工業用パイプ用です。 C-series は、密閉型薄肉チューブおよびインナービーズ酸化制御ターゲット用です。

関連

その他FYID-Feiyide 範囲のシステム。

お見積りはこちらからお問い合わせください

  • 5 stars: 1 (100%)
  • 4 stars: 0 (0%)
  • 3 stars: 0 (0%)
  • 2 stars: 0 (0%)
  • 1 star: 0 (0%)
A
Abhi M.
Oil & Gas High-Pressure Pipeline Welding

FXT machines are robust and reliable for high-pressure pipelines. They ensure safety, consistency, and excellent weld quality every time.

Frequently asked questions

  • What is the FXT40 Pro all-position pipeline automatic welding machine?

    The FXT40 Pro is an open-head orbital TIG system for industrial pipe joints. It uses a Siemens S7-200 SMART V3.0 PLC and can be paired with a selected K-series head and wire feeder. Confirm the head, material and welding procedure for the job.

  • How does the FXT40 Pro ensure weld quality in overhead and all-position welding?

    The FXT40 Pro configuration includes AVC arc-length control and OSC torch oscillation. Weld appearance and inspection results depend on the joint, material, procedure and inspection plan; no fixed radiographic pass rate is specified.

  • What pipe diameters and wall thicknesses can the FXT40 Pro weld?

    The K-series heads cover pipe OD 20–325 mm. The overall listed wall thickness range is 2–13 mm, but each head has its own OD and wall limits. Confirm the selected head against the pipe drawing.

  • What are the groove requirements for using the FXT40 Pro automatic welder?

    Joint preparation depends on the material, wall thickness and qualified welding procedure. Share the pipe drawing and fit-up requirements so FYID can confirm the groove and root-pass setup.

  • How much efficiency can be gained by switching from manual welding to the FXT40 Pro?

    The FXT40 Pro supports eight-zone parameter control with eight stages per zone. Actual productivity depends on joint geometry, procedure, operator setup and inspection requirements.

  • Do I need a senior welder to operate the FXT40 Pro system?

    The system can store up to 50 welding program groups. Operators still need training and an approved procedure for the selected material, head and joint.

  • Is the FXT40 Pro suitable for harsh industrial environments?

    The power source is rated IP21. The standard 380 V three-phase version outputs 10–400 A DC; the optional 220 V single-phase version outputs 10–300 A DC. The power source is air-cooled and the K-series heads are water-cooled.

  • What kind of after-sales support does Feiyide (FYID) provide for the FXT40 Pro?

    The standard complete-unit warranty is 12 months, excluding consumables and damage from improper operation. FYID offers lifetime technical support and 7×18-hour online support in English and Chinese. Common spare parts are normally dispatched within 48 hours; transit time depends on the destination.